To weld stainless steel, identify the grade and joint requirements, prepare a clean and consistent joint, select a suitable process and consumable, and control heat and shielding through an appropriate welding procedure. Inspect the weld face and root, then complete the specified surface treatment and testing. A smooth bead alone does not establish corrosion resistance or joint integrity.
For a thin 304L enclosure, the main concern may be distortion and appearance. A pipe carrying a corrosive fluid brings different questions: root protection, internal surface condition, inspection access and acceptance criteria. Start with those requirements before choosing TIG, MIG or another process.
What to establish before welding
The drawing and material records should answer these questions:
- What are the exact grades on both sides of the joint?
- What are the thickness, joint geometry and welding position?
- Can the welder reach the root, and can it be inspected afterward?
- What will the component contain or support, and at what service conditions?
- Which fabrication code, customer specification and acceptance criteria apply?
Where required by the job, a welding procedure specification (WPS) sets the permitted variables. Supporting procedure qualification demonstrates the joint performance within the applicable qualification rules; welder qualification addresses the operator's ability. These are different records. A certificate for the parent material does not replace either one. See TWI's explanation of welding procedures.
The grade family also changes the welding problem. “Stainless steel” is too broad a description for selecting a procedure.
| Material family | Typical examples | Main welding consideration |
|---|---|---|
| Austenítico | 304L, 316L | Commonly welded by several processes; control cracking risk, contamination and distortion. |
| Ferrítico | 430 | Heat-affected-zone grain growth and toughness require attention. |
| Martensítico | 410 | Hardening and hydrogen cracking can require controlled preheat and postweld treatment. |
| Proveedor de Acero Inoxidable | 2205 | Follow the specified thermal limits to preserve the required phase balance and properties. |
These are starting points, not interchangeable recipes. TWI's stainless steel weldability guide explains why grade-specific control matters. In particular, do not apply advice for common 304L sheet automatically to 410 or duplex material.
Which welding process should you choose
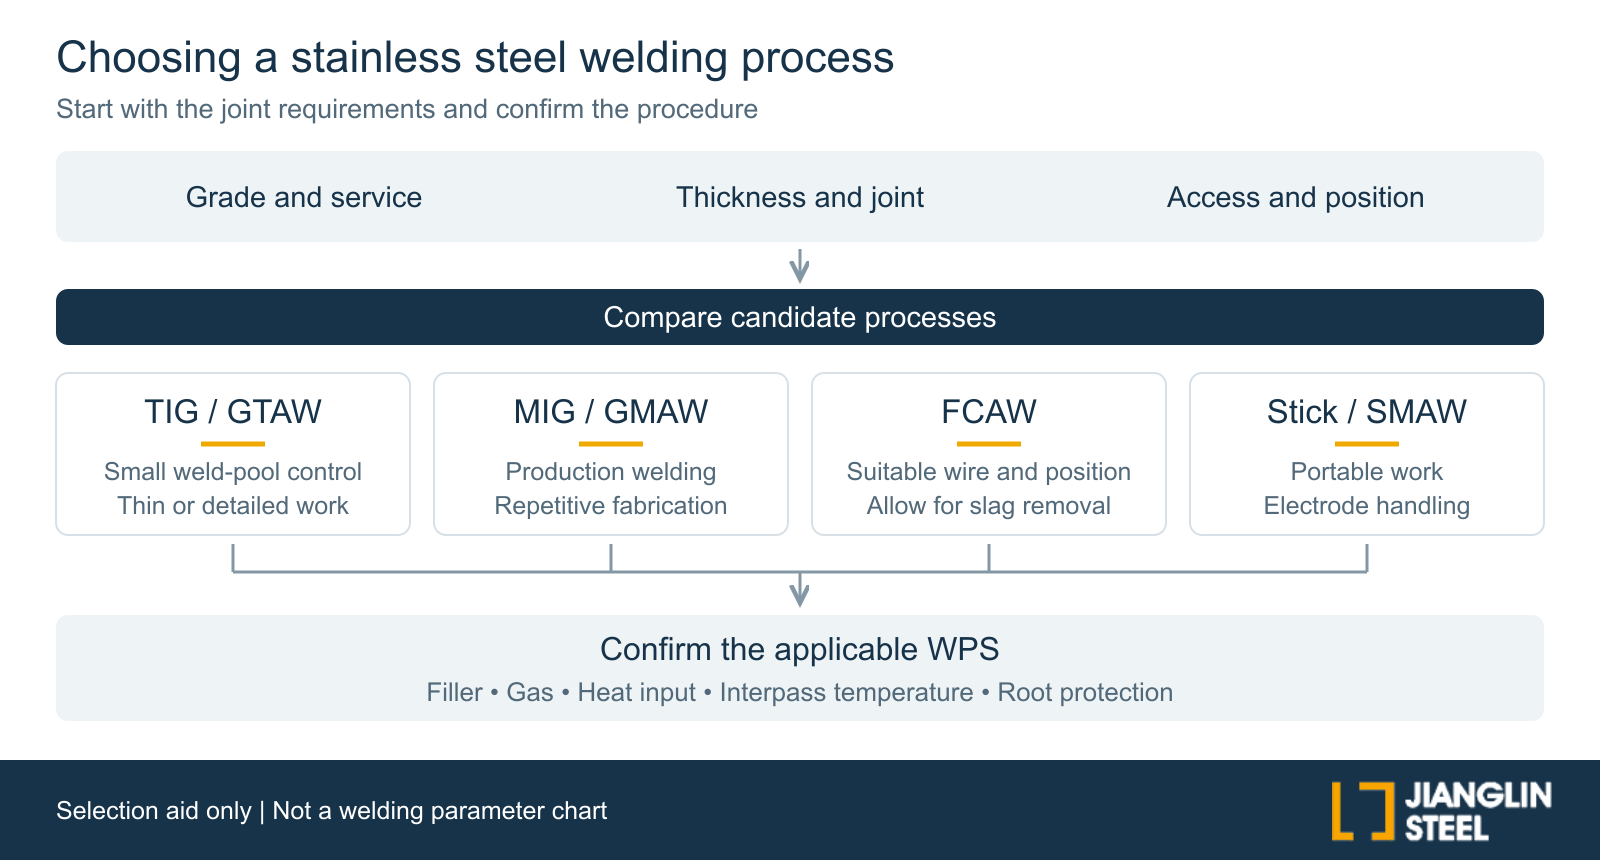
TIG is often considered when control of a small weld pool and a clean, precise joint are priorities. MIG can be attractive for repeat fabrication and higher deposition rates. Flux-cored and stick welding have other practical uses, but their consumables and cleanup requirements must suit the job.
| Proceso | Where it may fit | What to check before selection |
|---|---|---|
| TIG or GTAW | Thin sections, accessible pipe roots and detailed work | Joint fit-up, welder skill and the time needed to complete the weld. |
| MIG or GMAW | Repetitive fabrication and longer welds | Transfer mode, wire and gas compatibility, access and fusion. |
| Flux-cored or FCAW | Work needing suitable deposition and positional capability | Stainless wire classification, any required shielding gas, slag removal and thickness suitability. |
| Stick or MMA/SMAW | Repairs and work where portable equipment is useful | Electrode selection and storage, joint access, slag removal and procedure requirements. |
This comparison is a selection aid, not a ranking. Process capabilities and limitations are described in the worldstainless welding handbook.
For example, consider a thin enclosure with a long visible seam. Selecting a faster process does not settle whether the finished panel will remain flat or meet the appearance requirement. The trial joint should use representative thickness, fit-up and restraint. For thin sheet, TIG, pulsed TIG and suitable short-circuit MIG applications can help address burn-through and distortion, but still need correct technique and fusion. Miller's sheet-metal welding guide discusses these trade-offs.
Prepare the joint without introducing contamination
Keep the weld zone free of oil, paint, moisture and unsuitable residues. Use cleaning products approved for the operation, and allow the prepared surface to dry before welding. Grinding dust, carbon-steel brushes and shared handling equipment can introduce iron contamination that later appears as rust staining. Dedicated stainless-use tools and clean work areas reduce this risk. The IMOA guide to fabricating austenitic stainless steels covers contamination sources and surface restoration.
Fit-up deserves as much attention as cleaning. An inconsistent root gap changes the amount of filler needed and makes it harder to maintain penetration. Poor alignment can also leave an internal step that later cleaning cannot correct. Check the prepared joint along its length rather than measuring only at the two ends.
For production work, record how the parts are held and tacked. A joint that looks acceptable before welding may move as the tack welds and main weld contract. Treat the fixture and sequence as part of the process, not as last-minute corrections.
Match the filler and shielding gas to the procedure
Select the filler by the actual base-metal combination, service requirements and governing procedure. “Stainless wire” is not a complete specification. ER308L is a common example for welding 304L, and ER316L for 316L, but these examples do not cover dissimilar joints, every service environment or every qualification requirement. Miller's sheet-metal guidance gives these common filler examples.
Shielding gas is also process-specific. Argon is commonly used for TIG, while stainless MIG and flux-cored wires may require different gas mixtures. Do not transfer a TIG gas choice to MIG, or use a carbon-steel gas setup simply because it is already connected. Follow the wire manufacturer's guidance and the WPS together. Miller's stainless pipe welding guide explains the differences.
Before the first joint, verify the consumable classification, gas identification and relevant machine settings against the job record. After a change of wire or cylinder, repeat the check. This makes an incorrect substitution easier to catch before it becomes a batch problem.
Control heat without sacrificing fusion
Weld distortion results from uneven heating and contraction. Its extent depends on the material, joint design, fit-up, restraint and welding sequence. A larger-than-needed weld or excess root gap can increase the amount of shrinking weld metal. Clamping may control movement, but restraint can also increase residual stress; it is not a universal cure. See TWI's guide to distortion causes.
Use the weld size required by the design rather than adding metal “for safety.” Where the design permits, balanced joints and weld placement can reduce distortion. A continuous sealing weld must not be changed to intermittent welding merely to save heat. TWI's design guidance discusses these choices.
“Keep the heat as low as possible” is incomplete advice. Too little effective energy can leave poor fusion, while excessive thermal exposure can damage the result. Use the procedure's heat-input and interpass-temperature limits, not an unqualified internet setting.
This is especially important for duplex stainless steel. Its weld properties depend on a suitable balance of ferrite and austenite, so both the thermal cycle and consumable selection matter. TWI's duplex welding guidance should not be reduced to a blanket low-heat rule.
Plan root shielding before closing the joint
Before welding a full-penetration joint, establish whether the root needs back purging and how that protection will be maintained as the joint closes. Confirm the purge arrangement and any applicable monitoring requirements in the procedure. Internal access must be considered at this stage, not left until the outside weld is finished.
Do not omit root protection because a different wire or process can operate without conventional back purging under specific qualified conditions. Miller's pipe welding guide explains that distinction.
Set acceptance requirements before fabrication
Specify dimensional and weld-quality acceptance criteria, examination methods and coverage before fabrication starts. Agree how inaccessible roots will be examined and which records must be supplied. For the detailed inspection options, see our stainless pipe and tube NDT guide.
Keep the postweld surface-treatment requirement separate from weld integrity. Use our weld heat-tint guide for oxide-removal decisions and the passivation guide for treatment and verification requirements. Here, the planning task is to allow the access and processing steps those requirements need.
Plan for welding fumes and purge-gas hazards
Stainless steel welding can generate hazardous fumes, including hexavalent chromium exposure. Provide a site-specific risk assessment, suitable fume extraction and the required protective equipment. Shielding and purge gases can displace oxygen, particularly in enclosed spaces. Do not treat an inert gas as harmless or enter a vessel without the applicable confined-space controls. OSHA covers these hazards in its welding fume and gas fact sheet y hexavalent chromium guidance.
Preguntas frecuentes
Can 304 and 316 stainless steel be welded
Yes. Austenitic 304 and 316, including their low-carbon L variants, are routinely welded using suitable processes and procedures. Their filler and service requirements are not automatically identical, and “weldable” does not mean every weld will meet the required corrosion or mechanical performance.
Does stainless steel always need preheating
No. Common austenitic grades generally do not need preheat, while some martensitic applications require controlled preheat and postweld heat treatment. Identify the exact grade and follow the procedure. Do not apply one grade family's rule to all stainless steels.
Why are there no universal amperage and gas settings here
Thickness alone does not describe a weld. Joint geometry, position, wire or electrode size, process mode and material combination also matter. A parameter table without those conditions can be misleading. Use a procedure covering the actual application and validate changes as required.
Is TIG always better than MIG for stainless steel
No. TIG can suit work that needs close control of a small weld pool, while MIG can suit repetitive fabrication and higher deposition rates. The choice depends on the joint, access, procedure coverage and required result. A process name by itself is not a quality guarantee.
Bring the welding requirements into the fabrication brief
For a project discussion with Jianglin, provide the grade, thickness, joint drawing, service conditions and required inspection or surface finish. Refer to our custom stainless steel fabrication page for the broader fabrication context. Project-specific welding capability, procedure coverage and acceptance documents should be confirmed before an order is agreed.